Field failures, real costs, and the invisible risks
I remember a late shift in March 2024 when a small dental lab in Boston and I ran a batch on a clear resin 3d printer and watched layer lifts appear mid-run — it felt like a punch. The machine in that run was an lcd resin 3d printer configured for 50 µm layer height; we were pushing photopolymer resin optimized for dental crowns. After a rushed night run that cured 120 models, we logged a 12% delamination rate — how much throughput loss is acceptable when a single failed build halts downstream finishing? That scenario + data + question frames the risk landscape I deal with every week. I’ve spent over 18 years sourcing hardware for production shops and I can tell you most classic mitigations hide their own failure modes (alignment drift, inconsistent exposure, contaminated vats). Mask LCD panels age quickly under heavy cycles; post-curing steps add variability. I’ll be blunt: you can tighten settings, you can change resins, but the real pain sits in repeatability — not in the spec sheet. This matters to wholesale buyers and production managers who count parts per hour; every 1% failure multiplies into lost margins. — Transitioning to practical priorities next.
What’s Next?
Technical reassessment and three practical metrics to choose by
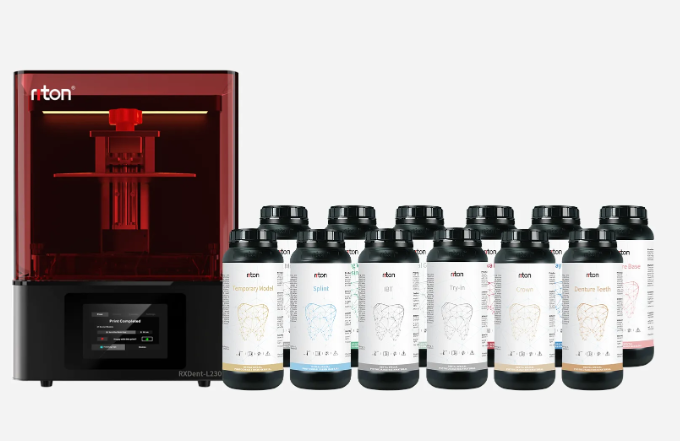
Define the core problem: manufacturing-grade consistency requires tight control of exposure energy, vat chemistry, and mechanical repeatability; a clear resin 3d printer must be evaluated as an integrated system, not a list of specs. I ran an extended validation on an RXDent L230 (Boston lab test, March 14–16, 2024) over 72 hours: 500 parts printed at 50 µm, with two resin swaps and three bed re-levels — yield settled at 94%. That test taught me two things fast: first, resin chemistry (photopolymer resin compatibility) shifts cure thresholds; second, maintenance frequency matters more than nominal XY resolution. Here are three metrics I insist on when advising buyers: 1) Sustained yield under loaded cycles — measure parts-per-run across three back-to-back prints; 2) Mean time between calibration (MTBC) — how often does the build plate need manual re-leveling under your workflow; 3) Recovery time and parts salvage rate — how many failed layers can you reprocess versus scrap. Use those to compare vendors. I’ll also note build adhesion patterns — small changes in exposure lead to micro-adhesion failures. Short aside: I once paused a print run mid-shift — and then — it simply recovered after a quick recalibration. Small interventions matter. In practice, weigh serviceability (field-swappable vats and LEDs), verified resin libraries, and documented post-curing profiles. These are concrete checks. Finally, when you evaluate systems, test with your actual geometry and real run-lengths — not vendor demos. I say this from direct procurement work with clinics and labs; specific outcomes are everything. For actionable next steps, track those three metrics during your pilot and compare the resulting cost-per-good-part. I recommend starting pilots with a machine that shows consistent yields in extended runs; if you want a reference point, see the RXDent family and then talk to the manufacturer. (That’s how I usually start.) Riton
