Introduction: A Shop Tale, Some Numbers, and One Weird Question
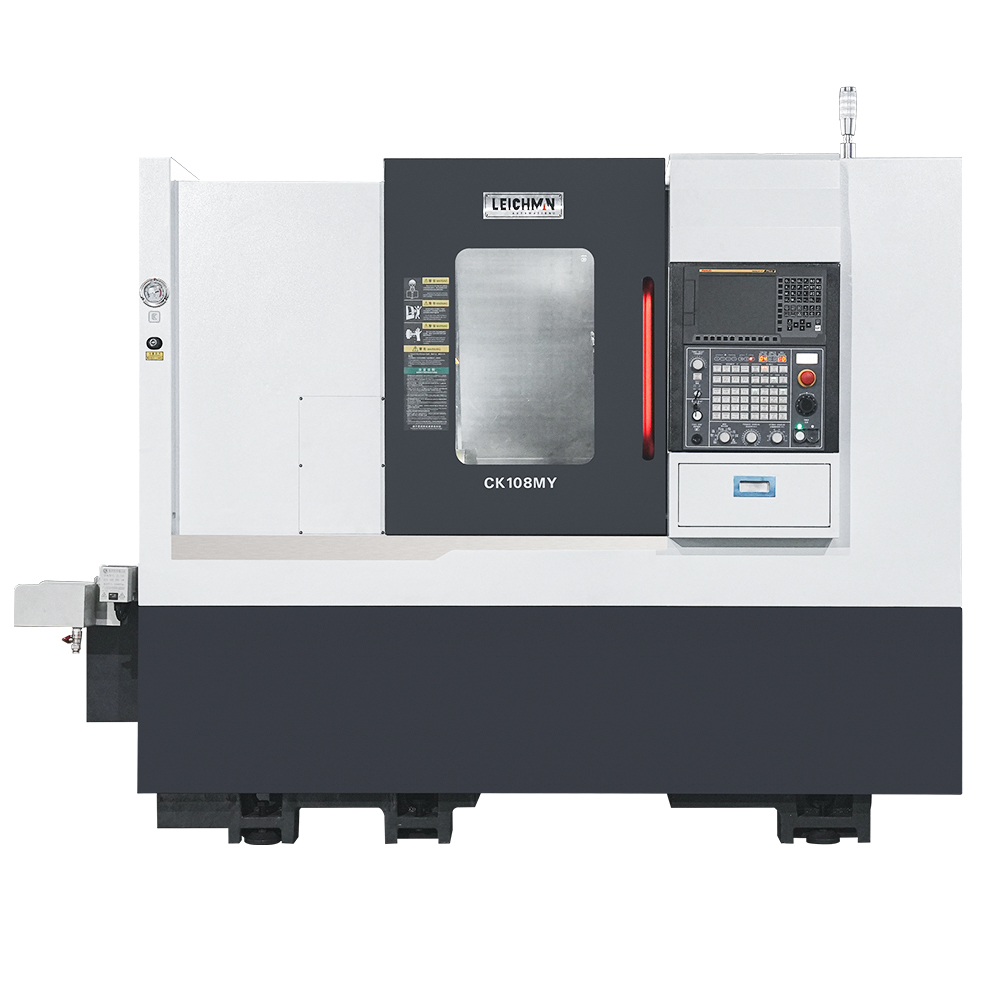
I once watched a machinist fix a jammed tool turret with a zip tie and a shrug — you learn quick on a busy floor. In the same week, our data showed a small shop cut cycle times by 18% after swapping firmware; yes, CNC milling and turning centers were the stars of that arc. So here’s what I keep asking: can a controller change how we think about production? (no, seriously — I mean it). I’ll be frank: I enjoy the drama of shop-floor surprises. They force us to question old habits, poke at assumptions, and laugh a little when a simple tweak saves hours. Next, I’ll dig into what usually hides under the hood — the annoyances and design choices that make or break a shift. — let’s move on and pull that thread.
Why the Usual Fixes Fall Short (and Where the Pain Really Lives)
When folks talk about upgrades, they often mean swapping parts or loading new code. But I want to point to a more stubborn problem: systemic mismatch. Consider the syntec control system cnc as an example. On paper, it promises tighter interpolation and faster probing. In practice, shops hit friction with spindle tuning, servo motor tuning, and old G-code habits that expect the machine to behave like yesterday’s lathe. Look, it’s simpler than you think: software and hardware must speak the same language, or you end up with jitter, missed offsets, and wasted time.
What’s the common failure?
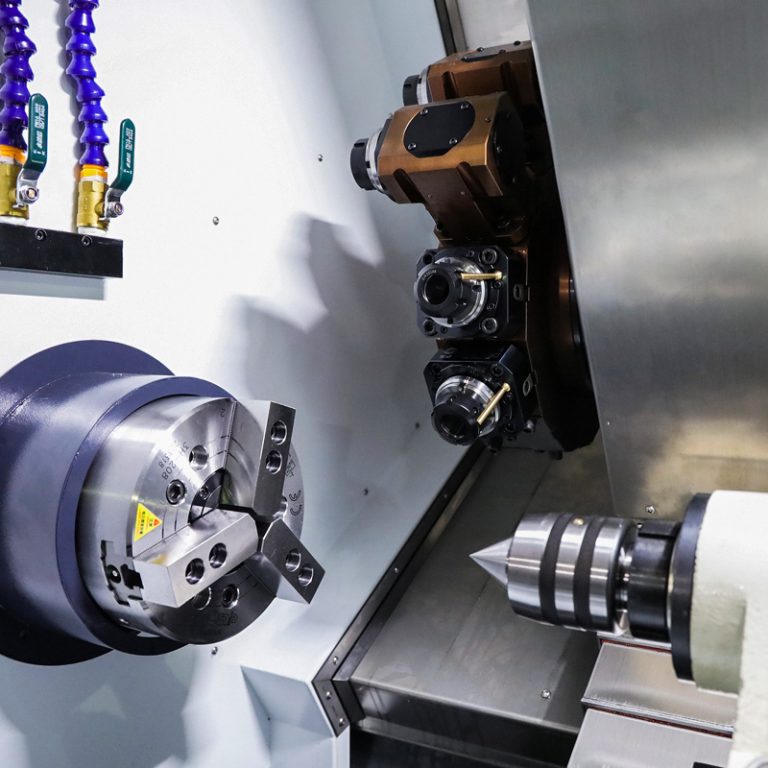
Two short points: first, vendor defaults often assume generic loads — which ruins fine finishes when your job is a thin-walled workpiece. Second, the human side: operators are used to hacks (manual offsets, trimmed feeds) that mask real problems. I’ve seen shops spend weeks blaming tooling when the issue was an under-tuned tool turret and a mismatched servo profile. It’s messy. And yes — funny how that works, right?
What’s Next: A Forward Look for CNC Milling and Turning Manufacturers
Now I want to look ahead. If we accept that controls are the pivot, then the next step is integration that respects both signal and skill. That’s why I recommend paying attention to data flow, not just specs. For example, modern setups can stream diagnostics to edge computing nodes for near-real-time adjustments. This reduces downtime and helps engineers tune power converters and feedback loops before a job goes wrong. For manufacturers, the choice is between boxed features and flexible, field-tunable platforms.
Real-world Impact?
Consider a mid-volume shop that embraced a platform-level change. They improved tool life and dropped scrap rates by refining spindle acceleration profiles and by enforcing tighter tool-change sequences. The effort involved training, yes — but the payback was clear: fewer emergency stops, more predictable runs. We measured throughput, but the bigger win was calmer shifts. Operators felt more in control. Productivity rose. Tools lasted longer. It wasn’t magic — just better matching of control logic to real work.
How to Choose: Three Metrics I Use Every Time
I’ll leave you with three practical metrics to evaluate any new control or upgrade. I use these because they cut through vendor marketing and get to what matters on the floor:
1) Response Consistency — Does the controller keep motion predictable across load changes? Test with step changes in spindle load and watch servo drift. 2) Diagnostic Transparency — Can you read real-time telemetry (temperatures, currents, encoder errors) without a proprietary black box? If not, you’ll be blind when things go sideways. 3) Field Tunability — Can you change PID gains, jerk limits, and tool-offset behavior without a factory service visit? If you need the vendor every time, expect delays.
Use these as filters. I’ve seen systems that score high on paper but fail on response consistency; conversely, humble controllers that give tight, controllable behavior win in day-to-day work. In the end, it’s about measurable gains: shorter cycle times, lower scrap, and fewer frantic calls at midnight — measurable and real. For sourcing and next-step demos, consider looking to trusted partners you can work with directly, such as Leichman.
