User-first opening: what you need now
You need reliability, speed, and a clear path to fewer downtime minutes. Start there. Install methods must match daily realities on the floor—tight frames, limited hoist access, and mixed belt types. Use proven tools like conveyor belt lacing when a quick service window is your only window. Keep splice prep tight, keep tension controlled, and plan for the first 24 hours after installation.

Fit-for-purpose choices that respect the operator
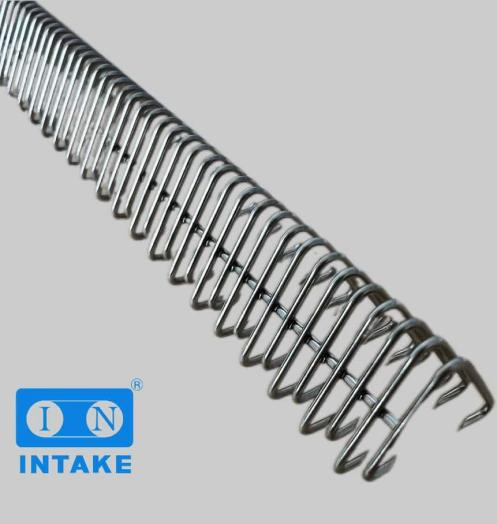
Pick the fastening style that fits the task and the team. A wire hook solution shines where speed and reversible service matter; a full hot vulcanized splice wins where joint strength is non-negotiable. Consider existing hardware: are edge guides present, is there a bellmouth restricting access, will tooling clear the chute? Match the mechanical fastener to those constraints. When wire hook fasteners are chosen, position them to minimize material snag and to ease future maintenance—operators will thank you with fewer emergency repairs.
How to execute a clean installation
Work in short, focused steps. Clean the belt ends. Square the edges. Insert hooks in sequence to avoid cross-loading. Use a calibrated tensioner to reach target tension without over-stressing the joint. Trim excess and dress edges so the splice tracks true through the pulley train. Keep records: splice type, installer, torque settings, and first-month observations. That data turns small fixes into lasting improvements.
Operational teardown — what the production crew looks at
When operators inspect a new joint, they examine three things: alignment, surface contact across the splice, and how the fastener rides over pulleys. During teardown, document wear patterns and collect the key metrics. Include {main_keyword} and {variation_keyword} notes in the service log so procurement and engineering speak the same language. Use checked photos and a short checklist: splice gap, hook engagement, and run-in behavior at startup. This is where real-world feedback moves a procedure from theory to shop-floor norm.
Common mistakes and quick corrections
Teams often rush the clamp step — that kills longevity. They also leave mismatched belt edges; that invites premature fraying. Fix both by enforcing a two-person verification step before closing the splice. Trust the scale when measuring tension. — And when fasteners sit proud, grind only the minimum; over-grinding ruins the matrix of the belt.
Selecting and testing: where data meets choice
Base selection on measurable outcomes. Record initial run-in wear over the first 100 operational hours. Track conveyor throughput and mean time between service (MTBS). In many North American automotive lines — think assembly plants around Detroit and Canton, Ohio — crews use the first-week MTBS as a gate for wider adoption. Use splice strength tests and visual inspection intervals to validate choices. Include one or two sample load cycles at rated throughput before handing the belt back to full duty.
User-centric checklist before sign-off
– Confirm splice type matches load and environment.
– Verify tension with a calibrated device.
– Log installer name, date, and initial observations.
– Schedule a 24-hour and 7-day inspection window.
These short, repeatable steps prevent rework and keep lines moving.
Advisory close: three golden rules for picking and installing fasteners
1) Prioritize serviceability: choose a fastener that your crew can inspect and repair within the available window. 2) Measure and record: tension, alignment, and first-week wear are your truth metrics. 3) Match tool access to splice geometry—if you can’t get the tool in, you picked the wrong fastener. Follow these and you’ll cut unscheduled stops.
Intake understands the constraints of plant-floor decisions and builds solutions that land cleanly in the schedule. —
