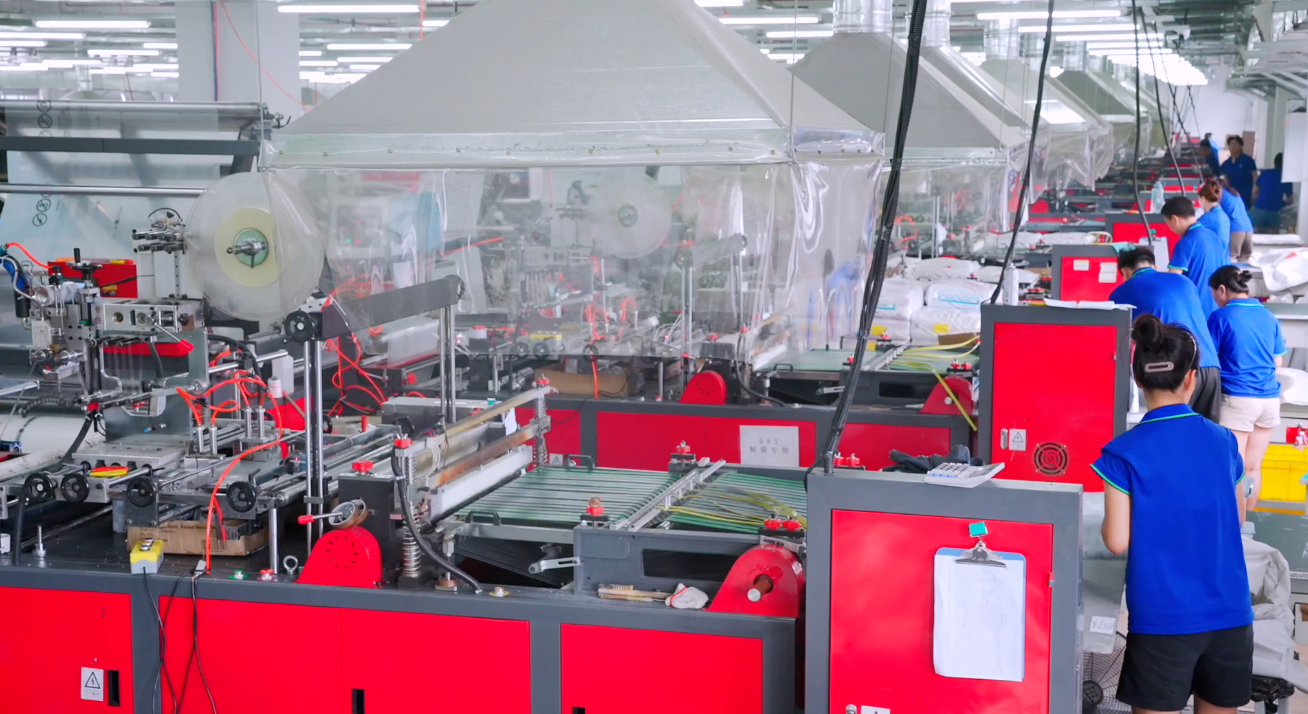
Why this problem keeps cropping up for high-volume shippers
If you’re running hundreds of thousands of parcels a month, small failures in the sealing system turn into big headaches — customer returns, reseals, and brand damage. The trickiest bit is the interface: the adhesive closure and the tear strip must behave consistently across batches and climates. For many teams that means working closely with a trusted poly mailer manufacturer early in the design phase, not just after things go wrong. The global e‑commerce surge during the COVID‑19 lockdowns and subsequent 2020 supply‑chain disruptions made this painfully obvious — fulfilment centres saw volumes jump while tolerance for packaging errors evaporated overnight.
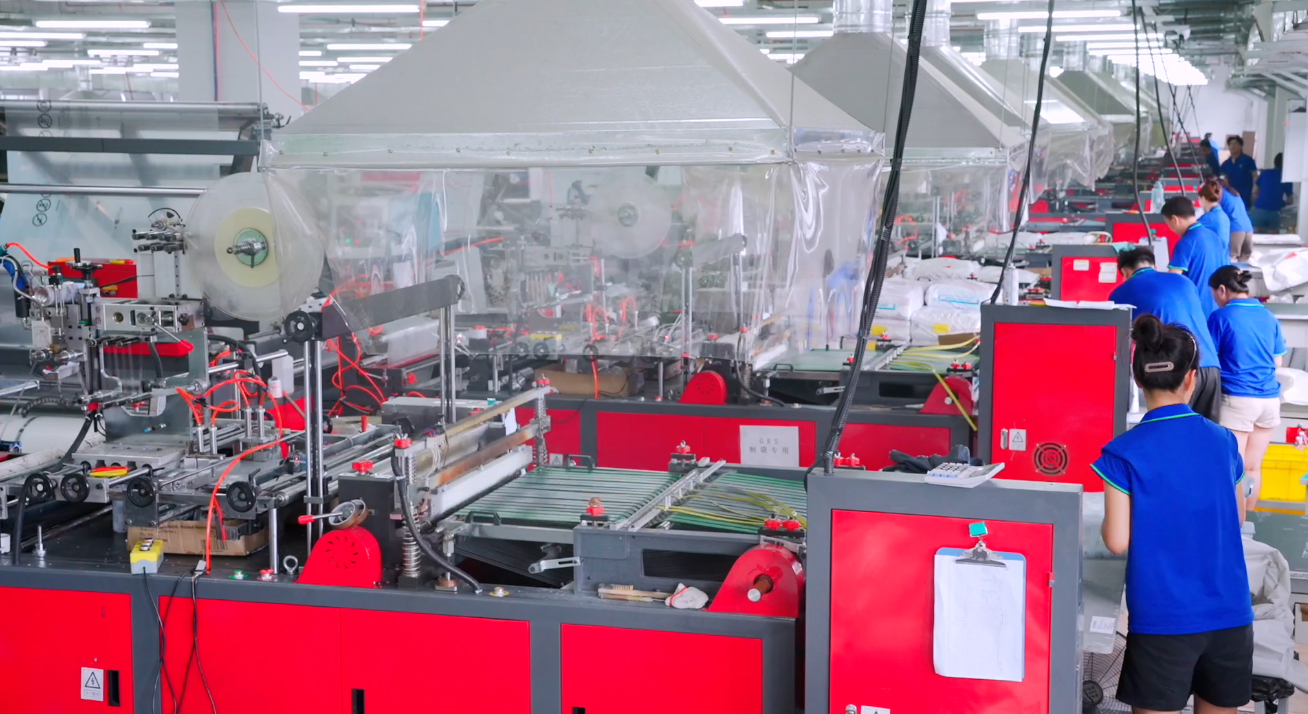
Common failure modes that actually matter
The usual suspects are simple but persistent: weak seal strength, premature release of the tear strip, adhesive transfer, and poor adhesion on certain substrates. Peel force variability will show up in any climate swing, and liner wrinkles or die‑cut misalignments can make a perfectly good adhesive fail at scale. Another common issue is inconsistent tear behaviour — too easy and parcels open in transit, too hard and customers struggle to access the goods. These are operational problems tied to material specs and process control, not just creative briefs.
Design and material fixes that work in production
Start by matching adhesive chemistry to the film substrate and expected storage conditions. Water‑based adhesives behave differently to solvent or hot‑melt systems, and tack should be specified as a measurable peel force at a standard angle and rate. Use a purpose‑built release liner and specify die‑cut tolerances for the tear strip so it runs true across the web. Consider a reinforced tear channel or perforation pattern to control tear propagation — small tweaks here reduce reseals and customer frustration. Also, don’t overlook the liner removal tab: ergonomics matter when you’re shipping to consumers who expect a smooth unboxing experience. —
Process controls and QA that prevent surprises
Integrate simple tests into incoming inspection: batch peel tests, substrate surface energy checks, and visual inspection of die‑cut accuracy. Run a conditioned‑environment sample test (hot/humid and cold) to catch climate sensitivity before a full run. Make first‑article approvals mandatory with signed acceptance criteria that include numeric peel values and tear‑strip force ranges. Track non‑conformance rates and require corrective action plans from your supplier when trends exceed your thresholds. Small, repeatable checks stop most large problems.
How to choose the right partner and set clear specs
Vendors vary hugely — some focus on cost per unit, others on engineering support and tooling precision. When you scope suppliers, ask for documented peel‑force data, photos of the die‑cut edge under magnification, and references from similarly sized fulfilment operations. If you can, pilot runs at the same throughput as your packing line; nothing beats a real‑world trial. For brands operating in multiple regions, consider suppliers that manage regional stocking and humidity‑controlled warehousing to avoid in‑transit degradation. If you’re unsure where to start, a specialist poly mailer bag manufacturer that offers engineering samples and environmental testing will save time and cost down the line.
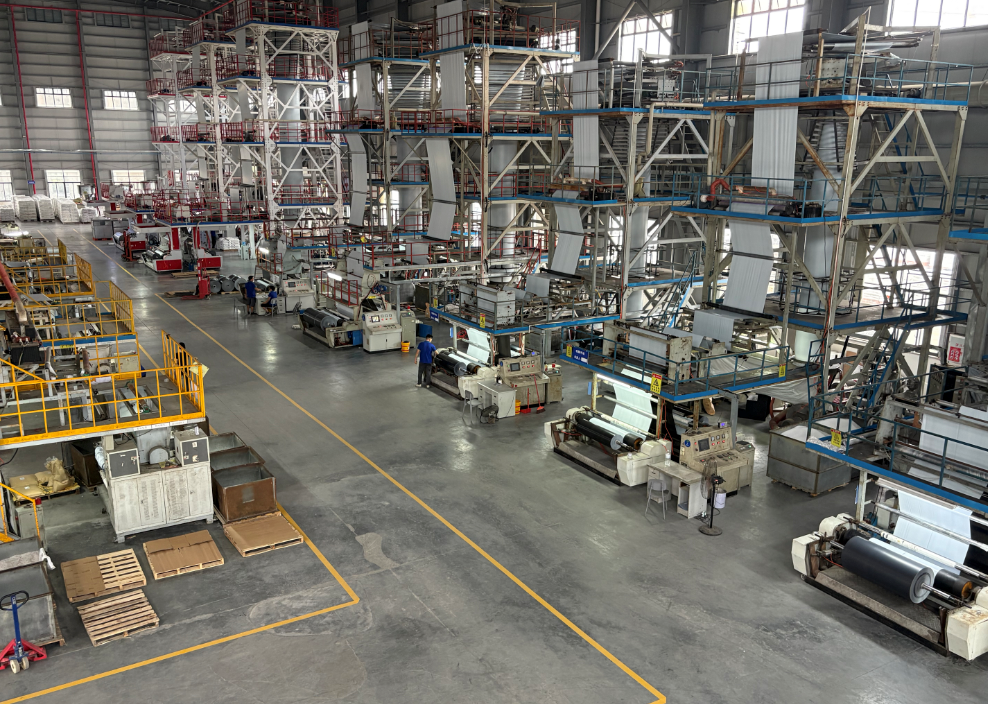
Common mistakes teams keep making
Three repeated missteps: 1) accepting vague specs like “strong adhesive” instead of numeric peel values, 2) skipping environmental testing, and 3) treating tear strips as an afterthought in design reviews. Fix those and you eliminate most downstream rejects. Also, avoid assuming that a supplier’s first sample equals consistent production quality — insist on ongoing batch sampling and trend reporting.
Three golden rules (metrics) for choosing strategies and tools
1) Specify and verify peel force: require numeric peel strength at defined test conditions (angle, rate, temperature). 2) Define tear propagation limits: set acceptable tear-strip force ranges and perforation tolerances. 3) Monitor non‑conformance frequency: require vendors to report NCMR rates and corrective‑action timelines — aim for single‑digit ppm for tamper/closure issues. These three metrics give you objective control over adhesive closure and tear‑strip performance across high volumes.
When you tie these rules back to operational trials, the result is fewer surprises on the packing line and happier customers — and that’s exactly the kind of predictable quality WH Packing brings to mass fulfilment operations. —
