Introduction — Scenario, Data, Question
Ever stood at the shop floor watching a part slowly emerge and thought, “Is there a faster, cleaner way?” I ask because I’ve seen weeks of lead time collapse into days when a single change clicks—the difference feels almost magical. In many shops, the CNC turret lathe sits center stage (noisy, proud, and stubborn), chattering through cycles while managers track takt time and scrap rates like hawks. Recent surveys show throughput gains of 20–35% after targeted upgrades; so my question is simple: what insight do we actually need to prioritize that upgrade? — and yes, I mean real, hands-on insight, not sales fluff.
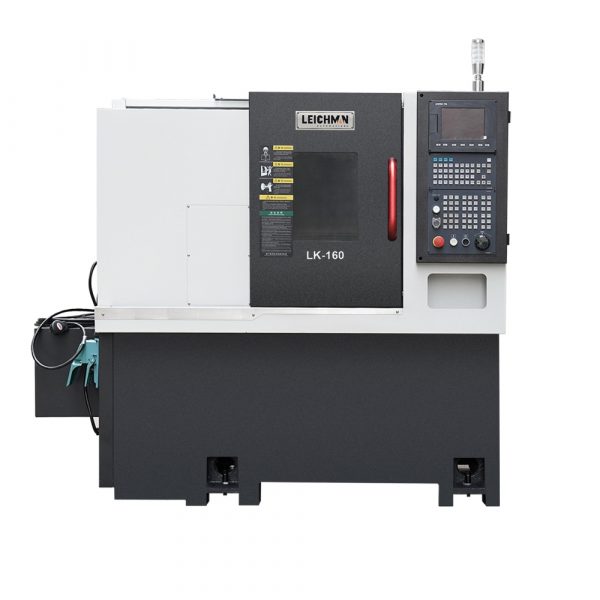
I’ll be blunt: I love machines, but I don’t love wasted minutes. The scenario is familiar: parts pile up, operators swap tools, and the work binds at choke points. Data tells us where the bottlenecks are—spindle speed mismatches, tool turret change delays, poor chip evacuation—but data alone won’t fix the human parts. So what do we look at first? This piece walks through the comparison, digs into the pain, and points to practical evaluation steps. Ready? Let’s move on — funny how that works, right?
Part 2 — Peeling Back the Layers: Flaws in Traditional Solutions
twin turret lathe setups promise throughput, but they often hide structural flaws that eat savings. I’ve seen twin turret systems sold as a silver bullet, yet shops still wrestle with misaligned tool paths, CNC controller quirks, and tool turret collisions that cheat cycle time. On paper, redundancy looks great—two turrets, more ops in one spindle—but in practice you hit issues like backlash, inconsistent live tooling performance, and complex fixture setups that negate expected gains.
Here’s a technical snapshot: when your spindle speed profiles don’t match tooling capabilities, you get chatter and poor finishes. When the CNC controller mapping is clumsy, programs grow brittle. Tool life drops because chip evacuation is subpar; operators spend time cleaning rather than cutting. Look, it’s simpler than you think: without intentional integration of drive systems and a tuned servo motor loop, the twin-turret advantage evaporates. We need to look past marketing specs and into real control loops, torque curves, and cycle-time studies.
Why does this still happen?
Because teams buy capability, not compatibility. They buy more axes but not better orchestration. They assume two turret heads automatically halve time — that’s wishful thinking. I’ve been there; I’ve pushed for changes and been frustrated by the slow wins. The right fix blends mechanical tuning, updated CNC firmware, and operator training so tool changes and live tooling sequences actually save seconds—seconds that add up to measurable throughput gains.
Part 3 — Forward-Looking: Principles and Practical Metrics
Looking ahead, I favor a hybrid of new technology principles and pragmatic shop-floor trials. If you’re evaluating a twin turret cnc lathe, don’t chase raw spec sheets. Instead, test integration: does the CNC controller coordinate both turrets smoothly? Can the system manage spindle speed transitions without dwell? Ask for real cycle-time demos and insist on seeing chip evacuation under load. These principles—control harmony, thermal stability, and robust chip flow—matter more than headline RPMs.
In practice, I recommend staged pilots. Start with a familiar part, instrument it, and measure before/after results. Use simple telemetry: spindle load, tool change time, and scrap rate. Then scale. The future won’t be about simply stacking turrets; it’s about system thinking: sensors, predictive maintenance, and modular upgrades that don’t require ripping out the whole line. — and yes, that takes planning and patience. We should be hopeful; incremental wins compound quickly when the control strategy is right.
What to measure next?
When you’re ready to decide, focus on three clear metrics. First, cycle-time reduction under real conditions (not ideal demos). Second, tool life improvement with live tooling under similar feeds and speeds. Third, net throughput per shift after accounting for setup and cleanup. These metrics give you measurable evidence. I’m biased toward shops that test for weeks and tweak relentlessly—because the returns show up on the bottom line.
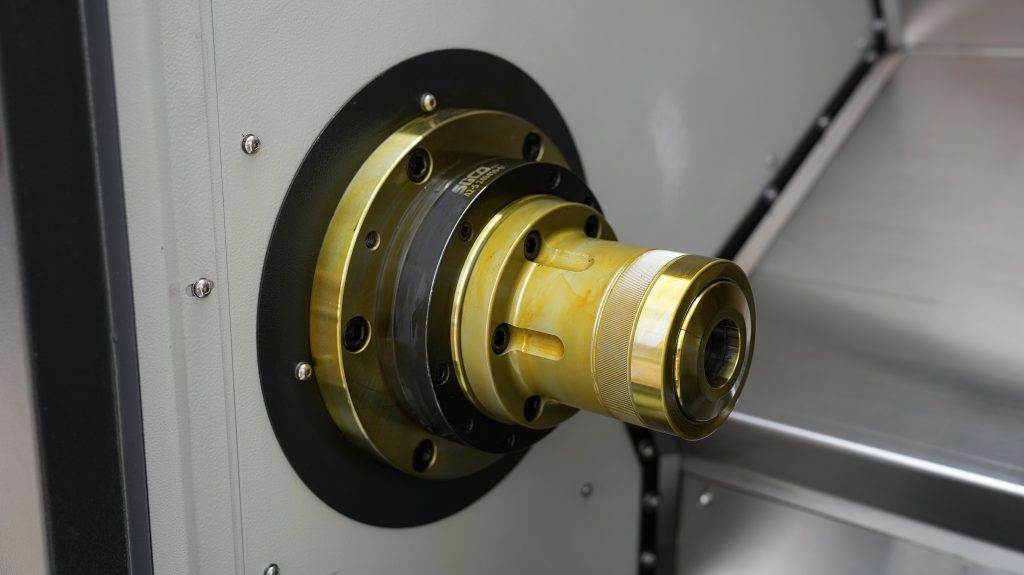
To wrap up, I’ll give you plain advice: don’t be dazzled by turret counts. Insist on compatibility, measure the right things, and factor operator workflows into every decision. I care about solutions that reduce frustration and deliver consistent parts — satisfying, isn’t it? For reliable machines and sensible guidance, consider brands that back demos with data. For example, check out Leichman for practical dual-turret options and documentation you can test on your floor.
