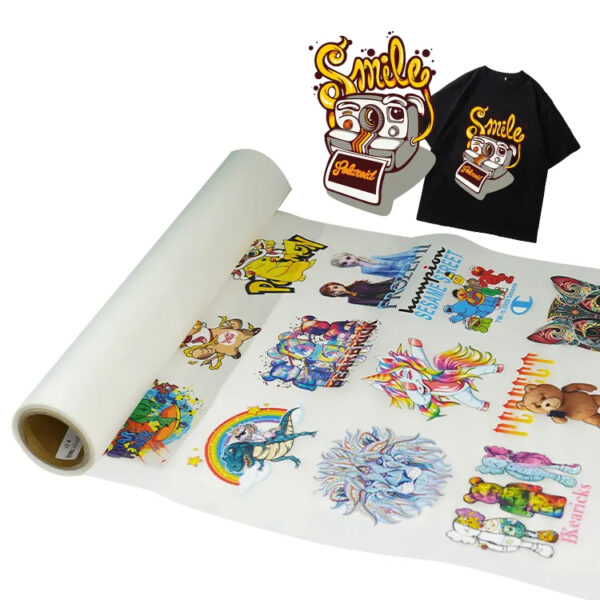
A Comparative Lens from the Press Room
Isn’t it odd how the same print looks perfect at noon and fragile at midnight? DTF Film keeps many promises, but it also reveals every weak link when the clock starts shouting. On a humid night in Shenzhen in June 2023, a 2,000-piece jersey run saw 7% edge lift after curing—what exactly failed? I phoned a trusted dtf film manufacturer at 10:30 p.m., and we traced the issue not to ink or ICC profile, but to the release liner’s silicone window closing up under heat. That small shift changed peel force, changed the whole job (aiya, that rush). Let’s move from noise to signals now—cleanly.
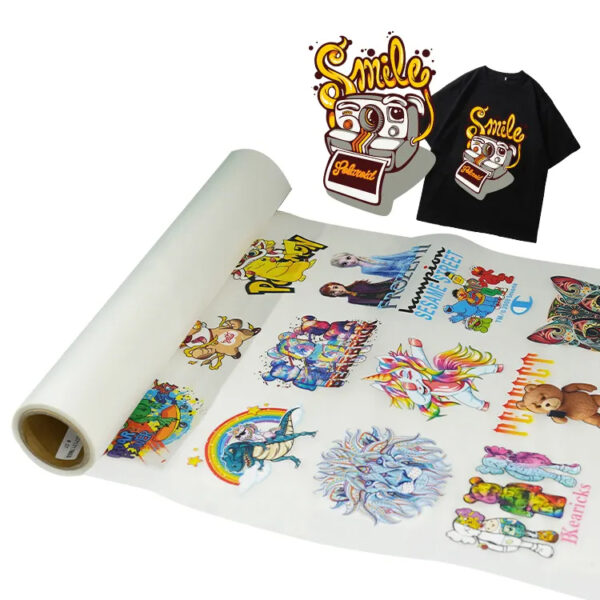
DTF Film Pain Points You Don’t See Until It’s Too Late
Where’s the real bottleneck?
I will be direct. The traditional fix—slow the press, increase white underbase, pray—only hides the real cause. In my fifteen years supplying teams from Guangzhou to Rotterdam, I see the same trap: operators tweak ink density and curing time while the PET carrier and hot-melt adhesive stay unexamined. When the carrier thickness tolerance swings ±5 microns, the melt flow changes. Then the adhesive pools around fine type, and line weight bloats by 0.2 mm. We blame the rip, but it is a materials problem. I once watched a crew shift from 140°C to 155°C curing to “lock it down.” Result: shinier finish, yes, but wash fastness fell after 10 cycles because the polymer over-crosslinked at the edges. Silent damage, very costly.
Another hidden pain point is the release liner’s silicone chemistry. If it is too tight, your cold peel becomes a tug-of-war; too loose, and half-tone areas lose cohesion. I tested two films the same afternoon—identical spec sheets, different peel windows. One let go at 35°C with buttery smoothness; the other needed 50°C and tore a 3 mm serif. All the while, operators kept pushing more white underbase to “stabilize” the transfer. That fix increases ink laydown, forces longer dwell, and risks dye migration on 150D polyester. In plain words: we treat symptoms, not causes. Yeah, I’ve done it too. The smarter path starts with the supplier’s process control, not your last-minute band-aid on press.
Looking Ahead: Choosing Film by Signals, Not Slogans
What’s Next
We can step out of the firefight. A forward-looking buyer compares films the way a mechanic reads a gauge—by data tied to use cases, not brochure gloss. I now ask every dtf film manufacturer for three things before we even sample: (1) Peel curve vs. temperature with standard white ink—show me the force drop from 60°C to 25°C; (2) Hot-melt adhesive rheology at 140–165°C—so I can match to fabric denier and surface energy; (3) Thickness uniformity map of the PET carrier—no averages, give me the histogram. With these, I can predict if a fabric with raised texture will crush dots or keep them sharp. Then it hit me—every “mystery” failure I logged in 2021 ties to one of those three charts, not the operator’s mood or a mythical humidity curse.
Let me sum it up without rosy lines. Traditional patches—more white, slower peel, hotter platen—borrow time and return reprints. The real leverage (small but strong) lives in film engineering: stable release liner chemistry, a consistent PET carrier, and a hot-melt adhesive that wets at the right window, not the widest one. If you need a quick filter for your next buy, use these three metrics: 1) Peel window clarity: document a smooth, repeatable cold peel across 25–40°C with no serif tear; 2) Adhesive behavior: verify wash fastness after 15 cycles at 40°C without gloss shift or edge whitening; 3) Carrier tolerance: demand ±3 microns thickness variance to protect microtext and 60 lpi halftones. Miss any one, and you will pay in scrap or returns—maybe not today, but when the press runs late and the phone rings. That is when the film you chose speaks the loudest—Xinflying.
