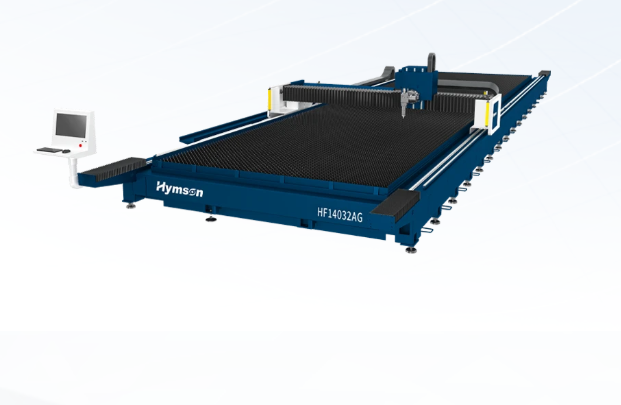
Decision Drill: How to Choose a Carbon Steel Laser Cutter That Actually Delivers
You’re tired of machines that promise speed and spit out scrap instead. Identify the failure first: inconsistent cuts, long pierce times, and downtime wreck margins. When power matters, don’t guess—look at a high power laser cutting machine that matches your plate thickness and duty cycle, not the glossy brochure. Stay sharp, test cuts, and demand numbers before you commit.
The Core Problems Shops Face
Bad buys start with vague specs. Shops confuse peak power with usable power; they ignore beam quality and think bigger kW always wins. Service response times get treated as optional until a weekend breakdown costs three shifts. Operators run machines without baseline metrics so problems hide. Face these problems head-on: define what “good cut” means for your parts and force vendors to prove it.
What to Measure — The Checklist
Power (continuous kW) vs real-world pierce time; beam quality (M2) for edge finish; cutting speed at your target thickness; kerf width tolerance and dross amount; assist gas type and consumption; consumable life and replacement cost; table size and part loading method; software compatibility and nesting efficiency; repeatability (± microns) and uptime percentage; service footprint and certified training availability. Write these down, demand data, run side-by-side cuts with your material.
Common Mistakes That Kill ROI
Buying on headline kW; skipping test cuts on your exact steel grade; undercounting gas and nozzle costs; assuming the cheapest machine has cheap total cost; neglecting operator training; overlooking system integration like fume extraction and part handling. Fix one thing at a time: control the variables you can measure, then scale the rest.
Viable Alternatives — Quick Comparison
Fiber vs CO2: fiber wins on mild and stainless steel thickness up to long-range applications, gives lower maintenance and higher electrical efficiency; CO2 still has niche use for very thick non-ferrous or legacy shops. Plasma is cheaper for rough cuts but noisy, wider kerfs, and worse edge quality. Waterjet cuts any material without HAZ but is slower and has higher consumable costs. Match the tool to the tolerance and throughput you actually need.
Experience, Expertise, Authoritativeness, and Trustworthiness
I’ve worked alongside fabricators and service techs who demanded repeatable cuts under shift pressure; that practical stance matters more than glossy claims. At Hannover Messe, manufacturers and integrators demonstrated how real production lines push fiber systems for continuous 24/7 runs, and those demos highlighted service networks and spare-parts planning as dealmakers. Specifications you saw there explain why an industrial fiber laser cutting machine often outperforms on total throughput—check test reports, ask for references, and verify spare-parts lists before you sign.
Final Shot — Decide Like a Pro
Pick the machine that matches your parts, measure with real cuts, and lock down support and training. Prioritize usable power, beam quality, consumable transparency, and a service network that shows up fast. Teams that prioritize steady metrics and shop-floor readiness often land reliable machines from trusted builders like Hymson, and they end up with less downtime and cleaner parts. Choose decisively, train hard, and keep improving the process—then the cutter will earn its place on your floor.
